How to Cut EPS Production Cost with a Recycling System
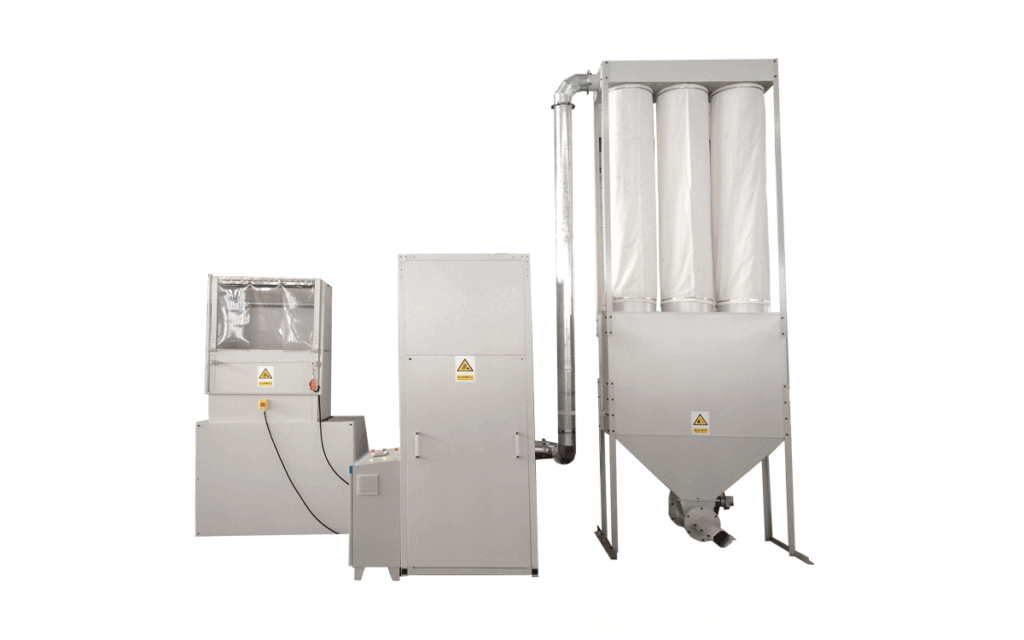
Raw bead is the largest single variable cost in an EPS plant, and a surprising share of it leaves the factory as scrap. Block ends, cut-offs, dust and rejected mouldings all add up. An EPS recycling machine converts that stream back into usable material, which is usually the fastest cost reduction available to an existing plant.
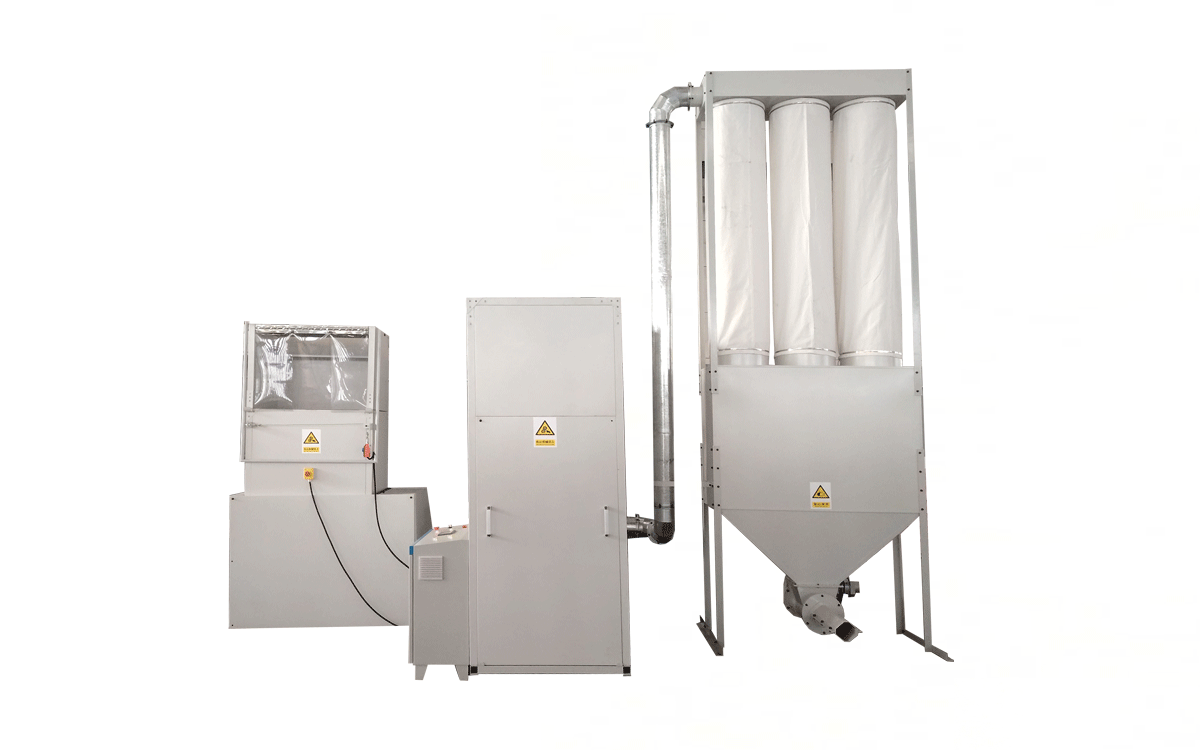
How the recycling system works
The system runs in three stages. A crusher reduces scrap to loose beads. A de-duster removes fines and dust that would otherwise cause surface defects and clog steam vents. A mixer blends the recovered bead with fresh raw bead at a set ratio. Plants running all three stages typically reuse more than 93% of their waste by weight.
Where the saving comes from
- Material — blending 5-15% recycled bead directly reduces raw bead purchases
- Waste handling — less volume to store, transport and dispose of
- Inventory — recovered bead acts as a buffer, so safety stock of virgin bead can be lower
- Quality — de-dusting removes the fines that cause weak fusion and surface roughness
What it means in practice
Take a plant consuming 100 tonnes of raw bead per month. At a 10% blend ratio, roughly 10 tonnes of scrap returns to production each month instead of being dumped. The saving is the bead cost plus the avoided disposal cost, and for most plants the equipment pays for itself within a year.
Keeping the blend safe
The blend ratio is not unlimited. Thin-wall packaging, fish boxes and appliance inserts need cleaner material and should stay near the lower end of the range, while insulation block can take more. Whatever the ratio, keep the recovered bead dry and free-flowing: pairing the unit with an silo system prevents bridging and keeps the feed consistent into the EPS pre-expander machine.
Send us your monthly scrap volume and product mix and we will size the right system — contact our team.
Sizing a recycling system in five steps
- Weigh your waste for two weeks. Do not estimate. Collect every stream — block ends, trim, dust, rejected mouldings — and record it by weight per shift.
- Separate by source. Cutting dust behaves differently from block ends, and contaminated material has to stay out of the blend entirely.
- Choose the blend ratio you can defend. Start near the low end for thin-wall and surface-critical products; move up only after trial blocks pass your own quality checks.
- Size the crusher to peak, not average. Clean-up shifts and rejected runs arrive in bursts. Throughput should absorb the worst day of the month.
- Decide where the recovered bead goes. Direct to the pre-expander hopper or into silo storage? Storage decouples recovery from production and keeps the blend ratio stable.
Which waste streams can actually go back in?
| Scrap type | Where it comes from | Recyclable? | Note |
|---|---|---|---|
| Block ends and trim | Cutting line, trimming station | Yes | Cleanest stream, highest recovery value |
| Cutting dust and fines | Hot-wire cutting, sanding | Yes, after de-dusting | Must be separated; fines cause surface defects and clog vents |
| Off-spec blocks | Moulding, density or fusion faults | Yes | Crush whole; check why they failed before blending back |
| Rejected shape mouldings | Shape moulding, packing | Yes | Remove inserts, tape and labels first |
| Wet or water-soaked material | Outdoor storage, leaks | Only after drying | Water in the blend causes steam faults and density drift |
| Oil, solvent or glue contaminated foam | Maintenance areas, laminating | No | Keep it out of the recycling stream entirely |
Common mistakes
Skipping the de-duster. Crushing alone returns fines to the process, and fines are what cause weak fusion and rough surfaces. The de-duster is not an optional extra.
Blending by eye. A shovel of recycled bead “about right” is how plants lose confidence in recycling. Use the mixer’s set ratio.
Raising the ratio too fast. Move up in small steps and pull trial blocks each time. Jumping from 5% to 20% overnight will show up in your reject rate before it shows up in your accounts.
Storing recovered bead outdoors. Moisture is the enemy. Keep recovered material dry and free-flowing, ideally inside a silo.
Frequently Asked Questions
What blend ratio is safe?
Typically 5–15%. Insulation block accepts more; thin-wall fish boxes and appliance inserts should stay near the lower end. Validate on your own product before you raise it.
Will recycled bead change the colour of my blocks?
A consistent, controlled blend should not. Visible variation usually means the ratio is fluctuating, not that recycling itself is the problem.
How much space does a recycling system need?
Crusher, de-duster and mixer plus working space around each. Send us your floor plan and we will place the three units in your layout.
Does recycling affect CE certification or product compliance?
Recycled content does not change the machine certification. Product compliance depends on your market’s rules for the finished board or package — check that with your customer.
What is the payback period?
It depends on bead price, scrap volume and disposal cost in your market. Send us your monthly scrap tonnage and we will work the numbers with you — talk to our engineers.
Where the numbers actually come from
A recycling business case has four inputs, and all four are measurable before you buy anything:
- Scrap tonnes per month — weighed, not estimated
- Recovery rate — the share of that scrap that becomes usable bead
- Blend ratio you can defend — set by what you make, not by what you hope
- Bead price and disposal cost in your market — both vary widely by region
Monthly saving is roughly scrap tonnage × recovery rate × bead price, plus the disposal cost you no longer pay. Set that against the equipment cost and you have a payback period your finance team can check. The blend ratio does not change the recovered tonnage — it changes how quickly that tonnage re-enters production.
Send us those four numbers and we will build the case with you, including the floor space and services the system needs.
Does adding recycling slow production down?
No, when the system is sized to your scrap volume and the recovered bead is stored rather than fed straight back. Bottlenecks appear when blending is uncontrolled, not when recycling is installed.
What maintenance does the system need?
Crusher screens and blades wear, de-duster filters need cleaning, and the mixer should be checked for build-up. All three are routine plant tasks.